Diodes and BJTs
A two-terminal semiconductor that allows current to flow one way but not the other.
Insulator.
Electrons saturate the holes in P, leaving no differential for the electrons in N to jump towards. Meanwhile, the extra electrons in N flow back to the battery.
Conductor.
Electrons saturate N, push into the depletion region, then jump across to the holes in P, which then return to the battery.
A large positive current is allowed to flow from collector to emitter.
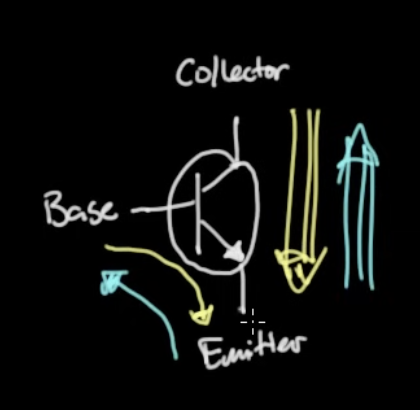
Image from Ben Eater's transistor video.
You're allowing electrons from the emitter to get all the way up into the base, so close that they can jump across the depletion region between base and collector.
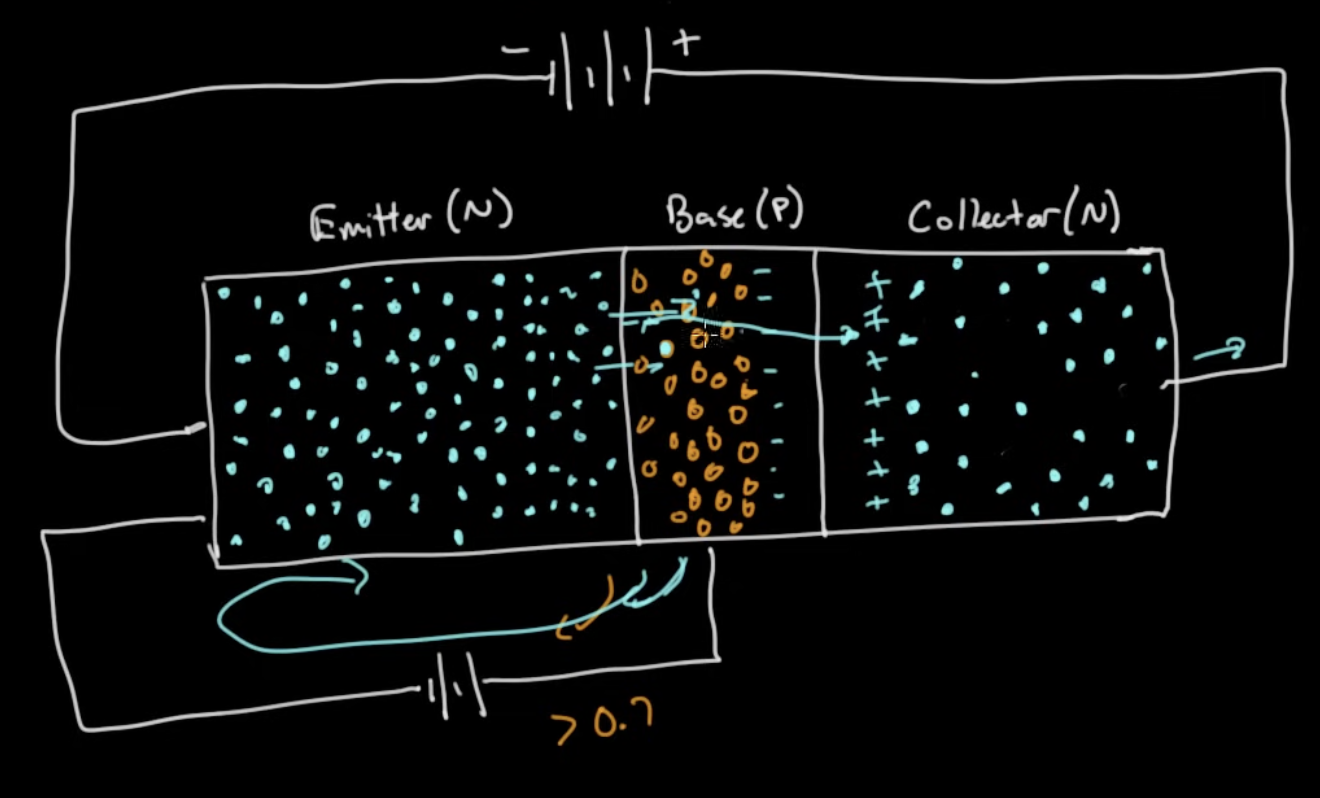
Image from Ben Eater's transistor video.
How a MOSFET works
Top to bottom: gate (metal) on top of an SiO₂ insulator, sitting on a P-type substrate. Two N-doped wells flank the gate on the left and right — the source and the drain. When the gate is positive, a channel of electrons forms in the substrate just under the insulator, connecting source to drain.
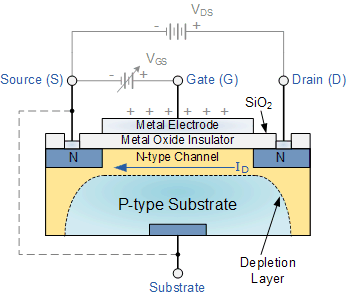
It pulls up the electrons in the P-type substrate, filling up the holes at the top — the channel.
When switching the device on, these doped regions supply the carriers (electrons or holes) to create the channel. Without the doping here, carriers would have to be generated by the silicon within the channel itself, which could take milliseconds or seconds.
In a MOSFET, the input is a voltage you set. In a BJT, it's a current you must keep feeding.
Thanks to the insulator between the gate and the channel, there's no power dissipated. The channel is powered just by voltage (basically potential energy).
When you turn the transistor on or off (i.e. when the gate voltage changes).
A capacitor.
Capacitance measures the ability of an interface to store charge. A higher capacitance means that a lower voltage can be used to store the same amount of charge.
A high gate capacitance means that the gate can effectively pull charge in or out of the channel to turn the device on or off.
In the context of wires, capacitance is bad because it causes charges in different wires to interfere with each other. This slows down signalling and therefore the clock speed of the chip.
What Intel learned from 10nm
- Cobalt interconnects. This material was complex to integrate and hurt yields.
- Multiple patterning. This increased the number of lithography passes and complicated the process substantially.
- Contact over active gate. This decreased the tolerance for misalignment and caused yield issues.
From planar transistors to gate-all-around
Its native oxide (GeO₂) is water-soluble and electrically defective. MOSFETs need a thin, stable, near-perfect insulator on the channel — only silicon grows one (SiO₂).
Dennard scaling refers to the period from 1960-2005 in which planar MOSFETs were scaled down by directly shrinking their dimensions, which increased power density.
However, threshold voltage and leakage current do not scale with transistor length - Source and Drain got so close together that they would be current even without the channel being on.
- Planar: gate sits flat atop the source-to-drain channel.
- FinFET: gate drapes the channel from three sides.
- Gate-all-around: gate fully wraps the channel from all sides.
Better gate control means you can shrink the source-to-drain distance (the "gate length") without source/drain fields leaking current through.
As transistors got smaller, silicon dioxide would let too much current leak between the gate and the channel. High K metal gates have better capacitance.
The gate consists of several metals that are chosen to optimize the conductivity of the gate and threshold voltage of the device. They can melt and degrade when subjected to high temperature processes that occur at the beginning of transistor fabrication. Therefore, they are deposited last to avoid these high temperature steps.
The first precursor gas is passed over the wafer. It typically has a metal part and an organic part. The metal portion binds to the surface, forming a single layer with the organic sticking up. This process is self-limiting because binding only happens between the wafer and the metal, not between the metal and the organic. Next, the chamber is purged and the second precursor is introduced. This gas reacts with the dangling organics pulling off the organic part of the molecule and leaving a single atomic layer of the metal. This process is repeated for as many layers as desired.
The inner spacer sits beside every sheet of gate material. It separates the gate from the source and drain regions. Its purpose is to make sure the source/drain are not connected to the gate, which would ruin the transistor.
To create the inner spacer, small crevices have to be carved out under the channel sheets. A liquid etchant would pull down these sheets due to the weight of the liquid as it dries. Therefore, a gas must be used to etch the crevice and avoid the pattern collapse.
More fab steps
In thermal oxidation, you're actually reacting with the silicon directly to make a new compound (Si -> SiO2) whereas in chemical vapor deposition, you're reacting some precursor gas to accumulate atop the existing material, not by turning it into something
Without the nitride atop to prevent thermal oxidation atop the corners of the trench, you'd create bonds there which are bent. Even once you mechanically polish them atop, they'd be vulnerable to mechanical stress, but with nitride atop they form clean molecular structures.
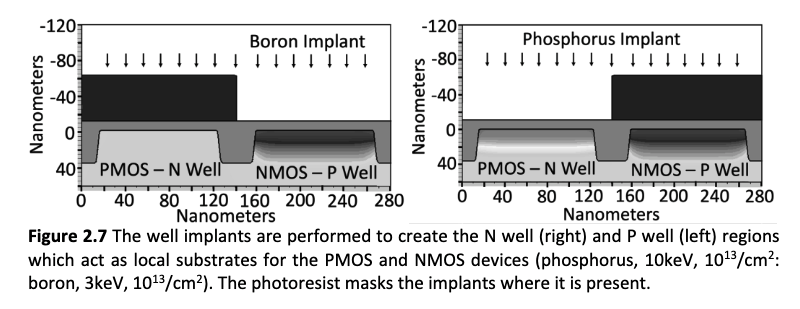
As the NA (the concentration angle) of the lithography increases, you have to use thinner layers of photoresist, lest you have inward sloping edges because of light angle. Thin resist can't block high energy well implants.
In dry etching, chemical reactants are shot at the wafer where they react and remove material. In wet etching, the wafer is submersed in a liquid etchant that removes material. Dry etching is typically more directional than wet etching.
A sample is made very thin (less than 100 nanometers). Then, electrons are shot at the sample. Different materials block or scatter the electrons by different amounts. These show up as darker or lighter regions in the image. This technique can visualize features down to the atomic scale.
EUV and High-NA EUV
Droplets of liquid tin 25-30 micrometers wide are dropped into a chamber where they are hit by two laser pulses. The first laser pulse reshapes the tin droplet into a flat sheet. Then, a second, higher power, pulse hits the droplet and vaporizes it into a plasma. The electrons in this plasma become excited and emit 13.5 nm light when they lose energy.
DUV masks are transmitting, meaning they selectively transmit or absorb light based on the pattern. Since every material absorbs EUV light, this approach cannot be used in the EUV case. Instead of transmitting, EUV masks must be reflective in the regions where the resist should be exposed.
1. EUV masks are reflective, so the blank mask must be made of 40-50 alternating layers of silicon and molybdenum. This structure is hard to fabricate. 2. Patterning the mask requires a dedicated multi-beam electron lithography tool. Inspecting the mask for defects requires another dedicated high-resolution inspection tool. Mask yield is ~50% which increases cost. 3. To keep dust particles off the mask, a pellicle must be placed over the mask which must be ultra thin and temperature resilient.
1. As the NA increases, the lenses become very large. Large lenses mean that the light will strike the lenses at a large angle. At large angles different polarizations of light are reflected differently. This reduces the contrast between the absorbing and reflecting parts of the mask. 2. The depth of field (DOF) quantifies what thickness of the resist is in focus during exposure. DOF ~ 1 / NA². Therefore, as the NA is increased, the DOF gets smaller, meaning a thinner resist must be used. Thinner resists are worse at blocking subsequent etching steps.
Replacing copper wires with ruthenium
Copper diffuses so much that if it was directly touching the transistor, you'd worry about it damaging sensitive areas. So we used Tungsten there.
Tungsten has higher resistivity, so it would require more power for all the interconnects if we used tungsten all over.
Ruthenium is easier to etch than copper, which allows you to etch out air gaps (air has the lowest capacitance)
At nanoscale, ruthenium has lower resistance, because mean free path of an electron is lower, which means it accumulates and thus dissipates less energy between collisions
- This allows air gaps to be created between interconnects. Air is a very good insulator, so this lowers the capacitance between interconnects when compared to having a dielectric there.
- It simplifies the process compared to making copper interconnects. Depositing and then etching ruthenium is easier than the Damascene process used to make copper interconnects.
Stacked transistors and 2D materials
2D materials improve the ability to turn the transistor on and off. Since the 2D material is very thin, the gate material is very close to the charges in the channel and can control them more easily.
- Making contacts to 2D materials is hard. Since they are so thin, the metal contact has to fuse with a thin layer of atoms, which is a difficult chemistry problem.
- 2D materials are very delicate. Their small thickness means small perturbations during manufacturing can ruin the material.
- Different materials have to be used for the NMOS and PMOS channels. There isn't a single 2D material that would work for both cases, so two different materials have to be used.
Hybrid bonding and packaging
In 2.5D, different chips are placed on an interposer. Connections between the chips are run through the interposer. In 3D, the chips are bonded directly to one another through solder bumps or copper connections.
Further reading
General semiconductor background
- How do Transistors Build into a CPU?YouTube
- Integrated Circuit Fabrication by Plummer and Griffinplummergriffinbook.stanford.edu
Gate-all-around transistors
Industry history and economics
- Intel’s Reign of TerrorYouTube
- The 3-D Transistor TransitionYouTube
- Intel Should Raise CapitalSemiAnalysis
Packaging
Fabrication technologies
- What ASML Has Next After EUVYouTube
- The Extreme Engineering of ASML’s EUV Light SourceYouTube
- Multi-Patterning Techniques: Enabling Dimensions Beyond Lithography Resolution LimitsYouTube
- Engineering the Gate-All-Around TransistorYouTube
- Applied Materials’ Pattern-Shaping TechnologyYouTube
- Embracing Chaos: The Imperfect Art of Semiconductor Manufacturing And LithographySemiAnalysis